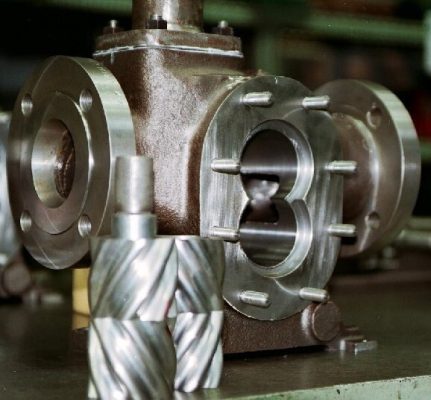





The confectionery manufacturing sector is a technically demanding field, particularly in the handling and transfer of raw materials. From thick molasses and glucose syrup to molten chocolate and cream or jam mixtures, each ingredient requires a specialized pump solution — one that not only delivers the required flow rate but also preserves product quality, structure, and hygiene. At Thái Khương Pumps, we are more than an equipment supplier; we are a technical partner, providing advanced pump systems tailored to every stage of candy and confectionery production, from raw ingredients to finished products.
Technical Challenges in Conveying Confectionery Raw Materials

Raw materials in the confectionery industry are extremely diverse and exhibit complex physical properties, placing demanding requirements on pump systems:
- High and variable viscosity: Many ingredients such as caramel, maltose syrup, concentrated sugar solutions, or liquid chocolate have extremely high viscosity, requiring pumps capable of handling them without loss of performance.
- Shear-sensitive: Particulate mixtures, creams, or gels can easily lose their structural integrity when subjected to high shear forces, affecting product quality and texture.
- Strict temperature control: Chocolate must be maintained at a stable temperature to remain in a liquid state. Other ingredients may solidify or change properties when temperature fluctuates.
- Hygienic requirements: All food-contact equipment must comply with high sanitary standards (CIP/SIP) to prevent bacterial contamination and ensure food safety.
Thái Khương Pumps’ Specialized Pump Technologies for Each Stage of Confectionery Production
Thái Khương Pumps offers a comprehensive ecosystem of dedicated pumps, carefully selected from reputable European brands, engineered to address every technical challenge in the confectionery production line.

OMAC (Italy) Lobe Pump: An Effective Solution for Ultra-Viscous and Shear-Sensitive Fluids
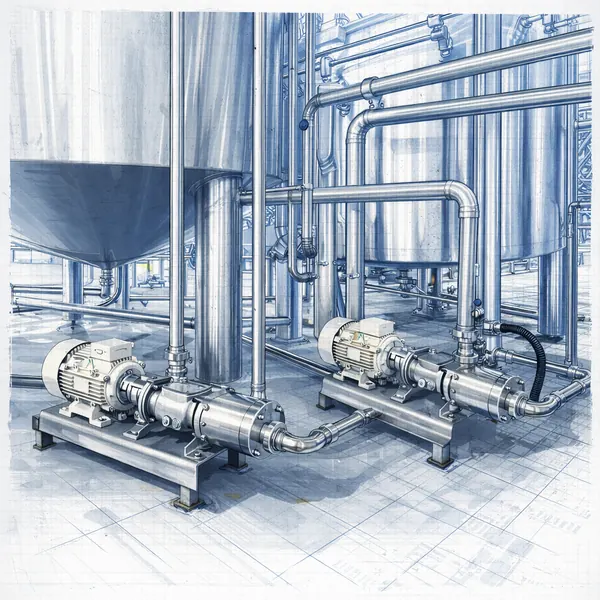
The OMAC lobe pump is a well-established choice for ingredients with extremely high viscosity and sensitivity to shear forces, such as gummy candy, thick syrup, chocolate, or cream fillings. The non-contact lobe design produces a gentle flow that preserves the structural integrity of the ingredient.
- High-grade materials: All wetted parts are manufactured from AISI 316L stainless steel with a low surface roughness Ra, meeting FDA food-grade pump and 3A Sanitary Standards requirements — easy to clean and resistant to product adhesion.
- Optional Heating Jacket: Models equipped with a heating jacket maintain stable temperature for chocolate or ingredients that must remain in a liquid state, preventing solidification.
- Smooth, gentle operation: Minimizes shear force, ensuring the final product quality is not compromised.
CSF Inox (Italy) Centrifugal Pump: High Performance for Low-Viscosity Fluids and CIP Systems
For mixing diluted sugar solutions, water, additives, or Clean-In-Place (CIP) cleaning operations, CSF Inox centrifugal pumps demonstrate notable advantages in performance and flow rate.
- Hygienic design: Optimized for Clean-In-Place (CIP) procedures, reducing cleaning time and improving production efficiency.
- Durability and efficiency: Ensures continuous, stable operation at low running costs.
Sanitary Diaphragm Pump: Flexible and Safe for Specialized Applications
Alongside lobe pumps and centrifugal pumps, sanitary diaphragm pumps are also a flexible solution, particularly for applications requiring high precision or handling mildly corrosive, slightly abrasive fluids, or fluids with suspended solids.
- Food-grade diaphragm pump construction: Typically manufactured from SS316L stainless steel with diaphragms made from PTFE (Teflon) or EPDM, ensuring chemical compatibility and hygienic integrity. The seal-free design eliminates the risk of leakage and contamination.
- Gentle transfer: Ideal for shear-sensitive fluids.
- Standards compliance: Our sanitary diaphragm pump range meets rigorous hygienic standards including FDA and 3A, making them suitable for a wide variety of confectionery applications.
Sanitary Standards and International Certifications: The Foundation of Reliability
The reliability of pump solutions in the food industry is built on strict compliance with international standards. Thái Khương Pumps is committed to:
- FDA and HACCP compliance: All distributed pump equipment meets or exceeds the requirements of the U.S. Food and Drug Administration (FDA) and Hazard Analysis and Critical Control Points (HACCP) principles, ensuring product safety.
- 3A Sanitary Standards certification: Many of our pump lines hold 3A certification — a recognized benchmark for hygienic design in the food and beverage industry.
- ISO 9001: Thái Khương Pumps operates under the ISO 9001 quality management system, from consultation and engineering through to supply and installation, ensuring every solution consistently meets a high standard of quality.
- Quality inspection process: Every product undergoes a rigorous quality inspection before delivery, accompanied by full CO/CQ documentation and a transparent warranty policy.
Real-World Case Study: Optimizing the Pump System at a Large Confectionery Plant
Thái Khương Pumps partnered with a reputable confectionery manufacturer in Vietnam that was experiencing serious pipeline blockage issues when transferring concentrated sugar solutions and molten chocolate.
Challenge: The existing pump system frequently encountered blockages due to the high viscosity and temperature variation of the ingredients, resulting in production downtime, increased maintenance costs, and reduced output.
Thái Khương Pumps’ solution: Following a thorough on-site survey and in-depth analysis, our engineering team proposed and implemented an integrated solution using OMAC lobe pumps with heating jackets for ultra-viscous ingredients, combined with an automatic temperature control system. We also optimized the piping layout and integrated dedicated Definox sanitary valves.
Results:
- Productivity improvement: A 30% reduction in cleaning time and a 15% increase in production line throughput, achieved by completely eliminating blockages.
- Cost reduction: System maintenance costs decreased significantly, saving hundreds of millions of VND annually.
- Quality improvement: Ingredients are transferred gently, preserving structure and flavor, thereby improving the final confectionery product quality.
This case clearly demonstrates Thái Khương Pumps’ experience and expertise in delivering comprehensive technical solutions that generate measurable economic and operational results for customers.
Why Choose Thái Khương Pumps for Confectionery Industry Pump Solutions?
With over a decade of experience in industrial food-grade pump applications, Thái Khương Pumps has consistently established itself as a trusted partner. We not only supply genuine imported equipment from reputable European brands but also provide:
- In-depth consultation: Our experienced engineering team will accurately analyze your technical requirements based on the properties of your ingredients and your production process.
- Optimized solutions: We design and deliver fully integrated pump systems that are economically efficient and deliver high operational performance.
- Lifetime technical support: We are committed to supporting our customers throughout the entire equipment lifecycle, ensuring stable and reliable long-term system operation.
Thái Khương Pumps is a strategic partner to many major domestic and international food groups, providing comprehensive Industrial Food Pump Solutions. We believe that specialized expertise and hands-on practical experience are the keys to delivering lasting value to your business.
Selecting the right pump system is a critical factor in determining efficiency and quality in confectionery manufacturing. With a thorough understanding of ingredient properties and production processes, backed by practical experience across many successful projects, Thái Khương Pumps is well-positioned to deliver specialized pump solutions that meet the most stringent industry requirements. Let us be your trusted partner, helping your business optimize production, improve quality, and achieve sustainable growth. Contact Thái Khương Pumps today for expert consultation and a comprehensive pump solution for your plant.